Why Factory Smartization Is No Longer a Choice, but a Necessity
In today’s competitive industrial landscape, manufacturing plants face major challenges such as fluctuating energy prices, high equipment maintenance costs, human error, and the constant demand for increased production speed. Traditional factory management methods can no longer keep up with high-volume operations.
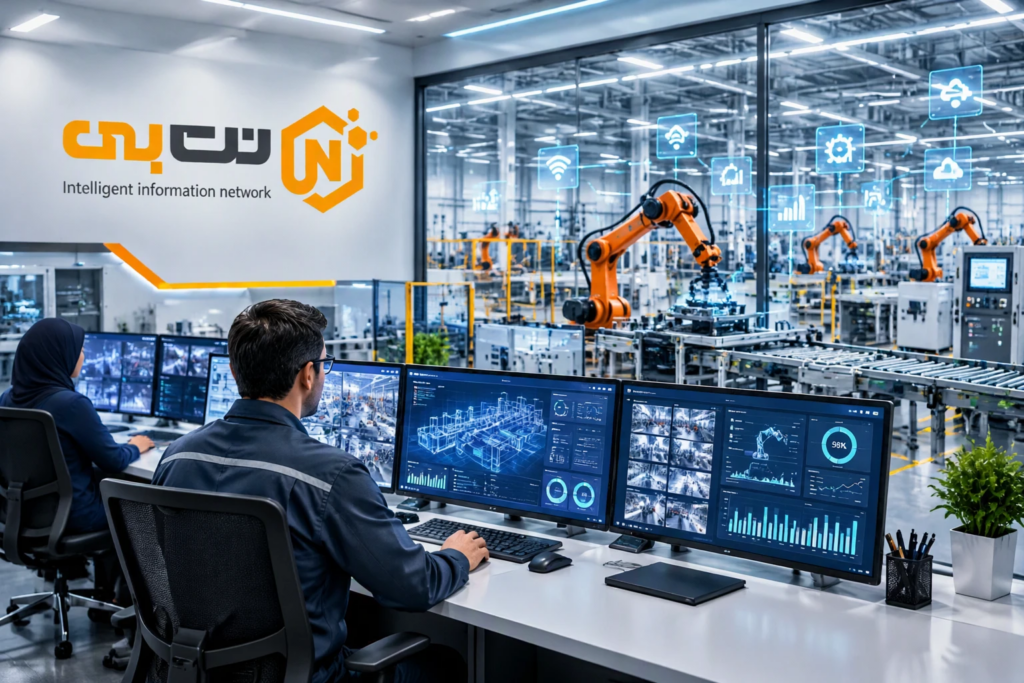
Factory automation and the implementation of the Industrial Internet of Things (IIoT) empower managers to maintain precise, real-time, and comprehensive control over all production lines, warehouses, and facilities. The advanced NetBee platform integrates all sections of your factory into a unified hardware and software ecosystem via a single dashboard, enabling data-driven, real-time decision-making.
7 Key Benefits of Factory Smartization with NetBee
1. Unified Monitoring and Centralized Control Dashboard
Managing fragmented factory sections has always been challenging. NetBee consolidates data from all production halls, boiler rooms, warehouses, and electrical substations into a single integrated dashboard, enabling real-time supervision via control rooms, mobile devices, and web-based systems.
2. Smart Energy Management & Cost Reduction
Energy is one of the highest operational costs in industrial units. The NetBee system continuously monitors energy consumption across every zone and device, automatically shutting down equipment when idle, managing peak loads, and optimizing the performance of furnaces, chillers, and compressors—leading to a dramatic drop in utility bills.
3. Predictive Maintenance
Sudden equipment failure halts entire production lines and causes heavy financial losses. NetBee’s high-precision vibration, temperature, and electrical current sensors detect early signs of wear or component failure before a complete breakdown occurs, triggering instant alerts.
4. Facility and Boiler Room Automation
Controlling temperature, pressure, and humidity in production halls, raw material warehouses, and server rooms is critical. By connecting to motorized valves, inverters, and HVAC systems, the NetBee platform maintains environmental conditions precisely within standard thresholds.
5. Industrial Perimeter Security and Access Control
Safeguarding the factory perimeter, warehouses, and sensitive areas is achieved by combining CCTV cameras, optical beams, motion sensors, and automated license plate recognition (ANPR) at gates. Furthermore, access levels for managers, operators, and staff are strictly segregated and logged.
6. Real-Time Emergency Response & Alarm System
In the event of industrial gas leaks, unauthorized furnace temperature spikes, electrical short circuits, or smoke in the warehouse, NetBee instantly activates local alarms, shuts off emergency valves, and sends push notifications or SMS alerts to the technical team.
7. Network Infrastructure Stability and Scalability
An industrial communication infrastructure must withstand harsh environments and electrical noise. NetBee guarantees 100% system reliability by supporting standard industrial protocols and secure IoT isolation networks.
Comparison Table: Traditional Factory vs. NetBee Smart Factory
| Evaluation Index | Traditional Factory | NetBee Smart Factory |
|---|---|---|
| Equipment Monitoring | Periodic manual inspections & paper reports | 24/7 real-time, smart, and automated monitoring |
| Energy Management | Discovering energy waste after receiving heavy utility bills | Real-time consumption analysis & automated electrical load optimization |
| Maintenance | Breakdown repair after failure occurs | Predictive maintenance (preventing failures before they happen) |
| Facility Control | On-site operators and manual switch adjustments | Full automation via scenarios, sensors, and artificial intelligence |
| Incident Response | Delayed and dependent on security/staff physical presence | Instant hazard detection, automatic emergency valve shutoff & rapid alerts |
Implementation Steps for Smartization in Industrial Units
- Energy Audit & Assessment: NetBee experts inspect production lines and boiler rooms to identify critical energy consumption and wear-and-tear hotspots.
- System & Network Architecture Design: Developing a comprehensive hardware (sensors, actuators, controllers) and software blueprint tailored to the factory layout.
- Industrial Installation & Wiring: Installing temperature, pressure, and vibration sensors, smart meters, and control panels without completely shutting down production lines.
- Central Dashboard Setup & Rule Definition: Integrating equipment into the NetBee platform and configuring automation scenarios and alarm triggers.
- Staff Training & Final Handover: Training operators and shift managers, running final system stability tests, and providing ongoing technical support.
Frequently Asked Questions (FAQ)
Does smartizing a factory require stopping production lines?
No. NetBee’s wireless or modular sensors and equipment are designed to be installed without long-term production halts, easily implemented during regular maintenance windows.
Can the NetBee system operate without an internet connection?
Yes. NetBee’s local gateways guarantee complete system independence. All scenarios, internal monitoring, and safety systems continue to operate seamlessly even during internet outages.
How much energy can this system save in a factory?
Based on conducted monitoring, utilizing the NetBee smart energy management system can reduce electricity, gas, and equipment depreciation costs by 15% to 35%.
Conclusion & Expert Consultation
Factory smartization is an investment that delivers a rapid return on investment (ROI) by cutting energy costs, preventing unplanned production downtime, and boosting operational efficiency.
To receive expert consultation, a free assessment of your factory floors, and an estimate of required industrial equipment, get in touch with the NetBee engineering team:
- Website: netbee.online
- Social Media (Eitaa, Bale, Telegram, Soroush):
@netbsign